Costly Laser Welding Mistakes Your Team Must Avoid
Shops that switch to fiber lasers usually see immediate gains, but those gains can vanish just as fast when small mistakes creep into daily habits. The technology forgives less than people expect. Where a MIG operator can grind past a bad start, a laser weld exposes every shortcut in the fit-up, cleaning, and settings. Owners who track scrap rates often find their laser bench producing more rework than the older TIG station within a few months, not because the machine is worse but because the discipline around it drifts. This article walks through the mistakes that quietly drain profit from an otherwise capable operation. Each one is easy to spot once you know what to look for, and each has a straightforward fix your team can apply the same afternoon. Fixing them will not turn a rookie into a master, but it will keep your best welders from losing time to problems that should not exist in the first place.
Skipping Fit-Up and Cleaning Steps
The most common problem is not a machine setting but the way parts arrive at the bench. Laser processes need tighter joints than arc processes because the beam cannot bridge a large gap the way filler wire can under a MIG torch. If your fit-up leaves a two-millimeter valley, the resulting seam will show voids, cold spots, or full burn-through. Shops solve this by adding a simple fixture step to every job and by refusing to allow parts through until the joint gap is verified with a feeler gauge or a printed template.

Cleaning Is Not Optional
Oil, mill scale, and cutting fluid all react badly with a focused beam. They produce porosity, spatter, and inconsistent penetration. A quick wipe with acetone and a lint-free cloth adds thirty seconds per part and eliminates a category of defects entirely. Teams that store parts in open bins near a grinding station tend to underestimate how much airborne dust settles on prepared edges. Move preparation into a cleaner corner and the defect rate drops without any change to the laser welding settings themselves.
Wrong Power and Wire Feed Settings
Copying settings from an online forum or a vendor demo is a good starting point but a terrible finishing point. Every shop runs a slightly different material grade, joint style, and shielding gas, and each variable shifts the ideal power curve. Operators who commit to running a short test coupon at the start of each new material batch avoid the trap of assuming last week’s numbers still apply. The five minutes spent on a test coupon prevent an afternoon of rework on a hidden porosity issue.
Wire Feed Missteps
Wire feed rate has its own quiet failures. Feeding too fast produces cold welds that look acceptable on the surface but fail in a pull test. Feeding too slow leaves a concave bead that undercuts the joint edge. Train operators to run a bend test on the first sample from any new setup. It takes two minutes and reveals problems that a visual check misses. Log the tested settings in a shared notebook so the second operator on the next shift is not starting over.

Ignoring Gas Coverage and Angle Control
Shielding gas is the invisible variable that ruins otherwise perfect welds. A hose kink, a low tank, or a torch angle that pulls the gas curtain away from the puddle all cause porosity, discoloration, and long polishing cycles. Owners often assume the operator is watching flow rate, and operators often assume the shop manager checks the tanks. Assign one person to a weekly gas check and put a laminated card on the wall listing the correct flow rate for each material.
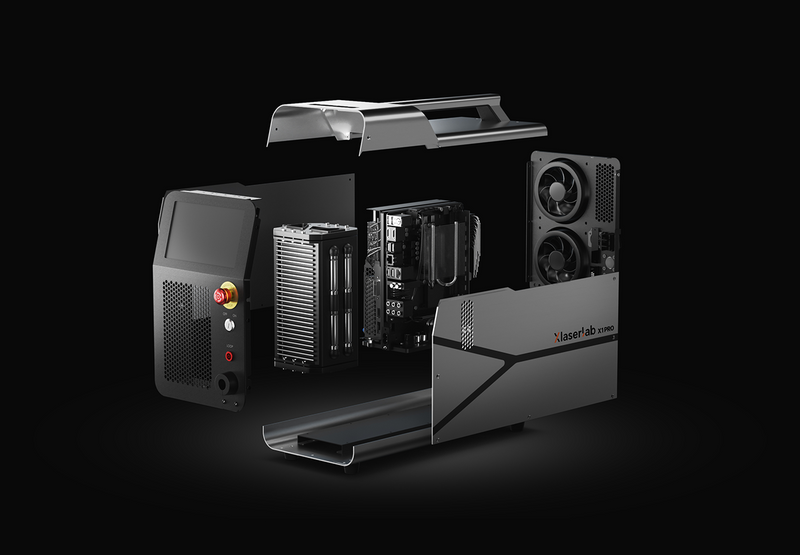
Angle control matters just as much. A laser head tilted more than fifteen degrees off vertical starts producing uneven penetration on one side of the seam. Xlaserlab handheld heads include an angle indicator on the grip, which helps new operators develop consistent muscle memory. Where indicators are missing, a mirror mounted at the end of the bench lets the operator self-check without stopping the run.
Overlooking Operator Training
A skilled arc welder is not automatically a skilled laser operator, and treating the switch as trivial creates a hidden training gap. The muscle patterns are different, the visual cues are different, and the failure modes are different. Shops that invest in a structured two-week onboarding, with sample joints signed off by a senior operator, avoid the slow decline in quality that otherwise appears three or four months after purchase.
Keep training documents short and practical. A single laminated sheet for each common joint, with photos of the correct and incorrect result, works better than a thick binder no one reads. Review the samples every quarter and update them as new products come through the shop. The goal is a shared standard that survives operator turnover and gives new hires an obvious target on day one.
Protecting the Investment Long-Term
Every mistake covered above shares a common root: a habit that made sense for arc welding but does not translate to a focused beam. The fix is never a new machine or a bigger power supply. It is a small operational adjustment, repeated until it becomes second nature. Shops that treat their fiber platform like a precision tool rather than a heavier version of MIG see the payoff quickly. Their scrap rate stays low, their finish times stay short, and their skilled operators stay engaged because they are not repeating the same problem week after week. Walk your shop tomorrow with this list in hand. Watch the first three welds of the day, check the joint gaps, and ask the operator to run a coupon on the newest material batch. That single hour of attention will likely save more money than any capital purchase this quarter.